
CNC Gantry Machining Center
CNC Gantry Machining Center
HPG (column moving) and SP (table moving) gantry machining centers engineered for large, heavy and high-precision parts.
A CNC gantry machining center (also called a double-column or bridge-type machining center) moves the spindle on a bridge spanning a fixed or moving table, delivering the rigidity and reach needed for oversized workpieces. HIRUNG builds two gantry families: the HPG series column-moving gantry for extra-large and heavy-duty parts, and the SP series table-moving gantry for high-speed, high-accuracy finishing. Both share HIRUNG Mechanite cast-iron construction, micron-level accuracy and globally proven CNC controls.
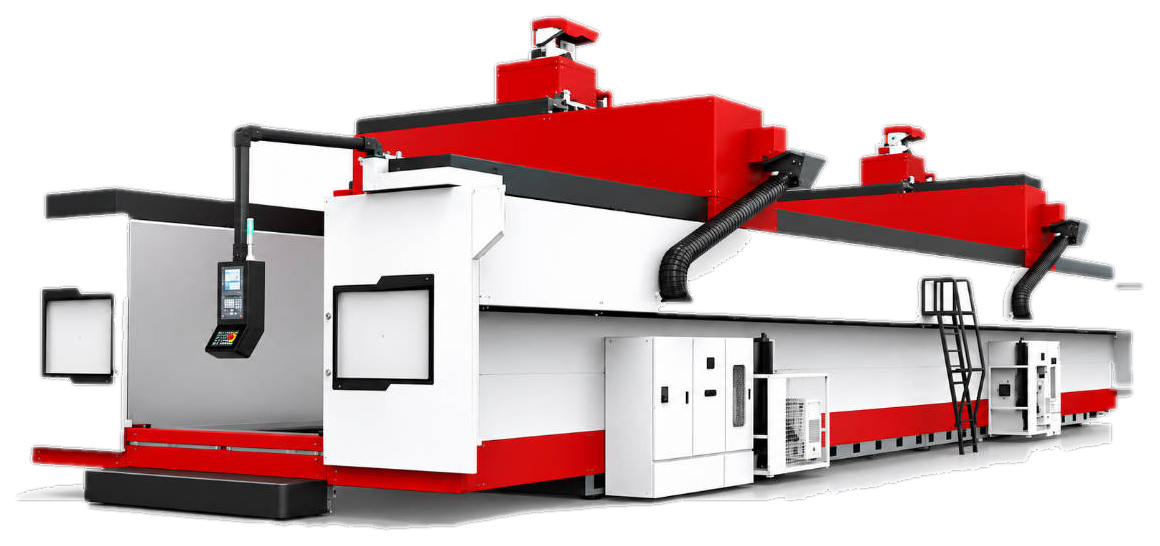
HPG vs SP
Two Types of CNC Gantry Machining Centers: HPG vs SP
Choosing the right gantry type starts with your workpiece weight, size and accuracy target. The HPG series keeps the table stationary and moves the column, so load capacity is effectively unlimited. The SP series fixes the bridge and moves the table, giving maximum damping and the best surface finish for precision molds and aerospace parts. The comparison below explains where each structure wins.
Column Moving
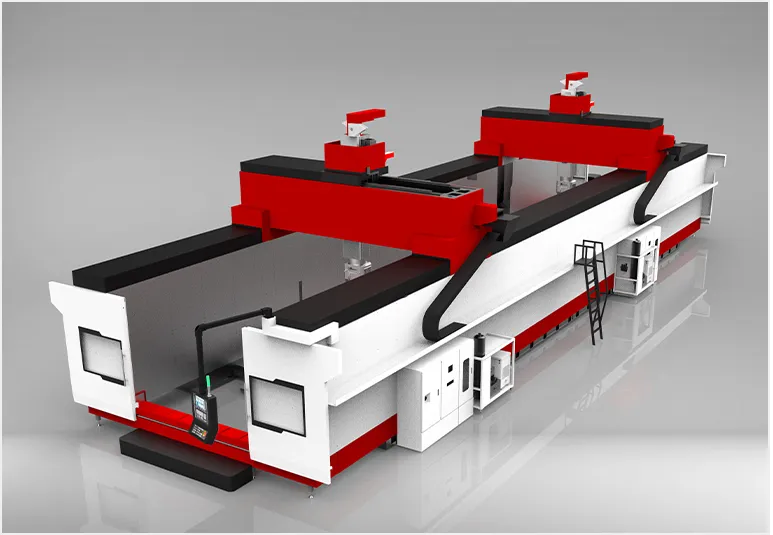
HPG Series - Column Moving Gantry
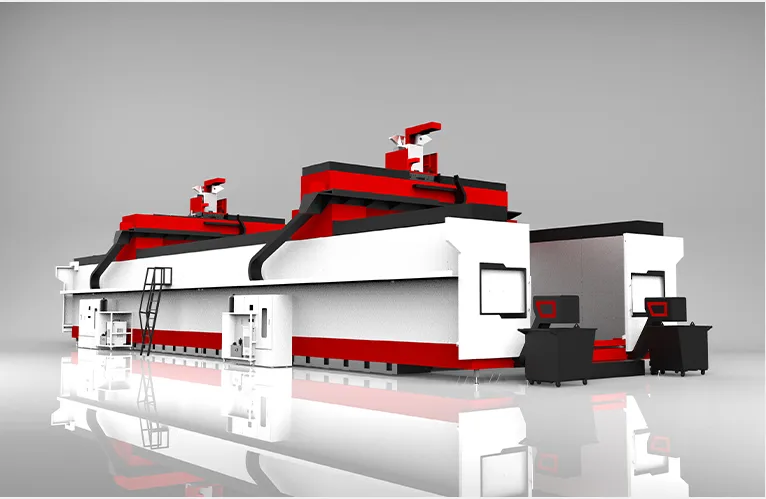
The HPG series uses a fixed table and a moving column (floor-type gantry). Because the table never moves, payload is effectively unlimited and the machine handles massive energy-equipment and shipbuilding components. Available in whole-style and split-style frames, with X-axis travel up to 12,000 mm as standard and custom lengths up to 60 m. Ideal when part weight and footprint dominate the spec.
Table Moving
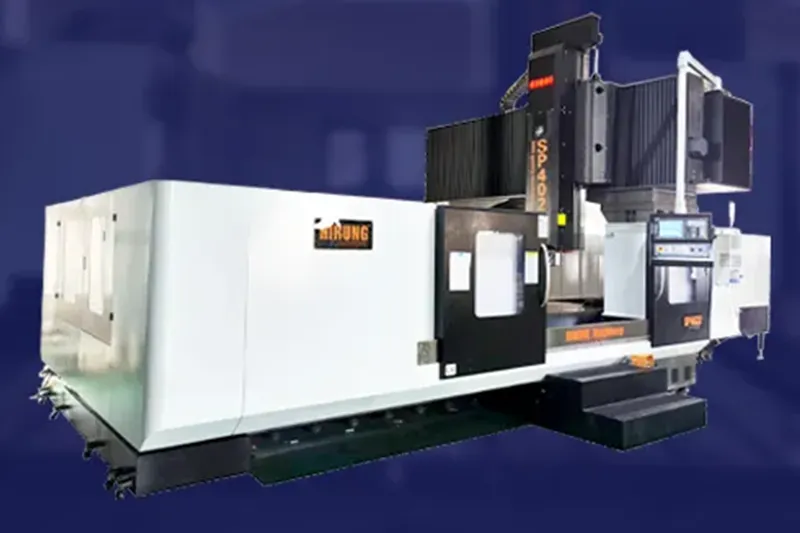
SP Series - Table Moving Gantry
The SP series uses a fixed bridge and a moving table, so the structure stays maximally rigid and damped during cutting. This makes it the natural choice for high-precision molds, aerospace structural parts and medical instruments where surface finish and repeatability matter most. Table load reaches up to 20,000 kg, with optional automatic angle heads for 5-sided machining.
HPG vs SP: How to Choose
| Factor | Table Moving (SP series) | Column Moving (HPG series) |
|---|---|---|
| Loading capacity | Limited by rated machine weight; workpiece must stay within design load (up to 20 t). | Practically unlimited – fixed table supports any weight that fits; motion is unaffected by workpiece mass. |
| Speed | Heavy load means labored motion, slower traverse and faster guide wear. | Consistent design speed regardless of workpiece weight – high speed, high efficiency. |
| Guide & accuracy wear | Varying heavy loads accelerate guide/screw wear – unstable accuracy, shorter life. | Constant moving mass – uniform, minimal wear; long-term precision stays stable. |
| Servo performance | Wide weight variation forces one reference weight – inconsistent accuracy. | Constant moving mass tuned once with load compensation – consistent high precision. |
| Machining accuracy | Table + part inertia causes lag (planetary drive) – precision hard to guarantee. | Fixed moving mass + X-axis dual-servo direct drive – reliable full-travel accuracy. |
| Floor space | Compact – same capacity needs under 60% of the column-moving footprint. | Larger footprint for equivalent capacity. |
| Workpiece scope | One part at a time (table always moving). | Secondary parts can be loaded or fixtured on the side during machining (safer, higher uptime). |
Specifications
HPG Series Specifications - Whole Style
| Model | Travel X/Y/Z (mm) | Table size (mm) | Max height (mm) | Spindle | Power | Rapid X/Y/Z (m/min) | Weight (t) |
|---|---|---|---|---|---|---|---|
| SP1810HPG | 2000 / 1050 / 550 | 1900 x 1000 | 730 | BT50 | 12/18 kW | 20 / 20 / 20 | 15.5 |
| SP2216HPG | 2500 / 1600 / 800 | 2200 x 1600 | 950 | BT50 | 16/20 kW | 20 / 20 / 20 | 25 |
| SP3016HPG | 3200 / 1600 / 800 | 3000 x 1600 | 950 | BT50 | 16/20 kW | 20 / 20 / 20 | 30 |
| SP4016HPG | 4200 / 1600 / 800 | 4000 x 1600 | 950 | BT50 | 16/20 kW | 20 / 20 / 20 | 33 |
| SP3020HPG | 3200 / 2000 / 1000 | 3000 x 2000 | 1150 | BT50 | 16/20 kW | 20 / 20 / 20 | 38 |
Note: Spindle: BT50, 8000 rpm belt (SIEMENS or FANUC). Control: SIEMENS 828D / FANUC 0i-MF. Models above are whole-style; split-style frames below extend travel and load.
Specifications
HPG Series Specifications - Split Style (customizable)
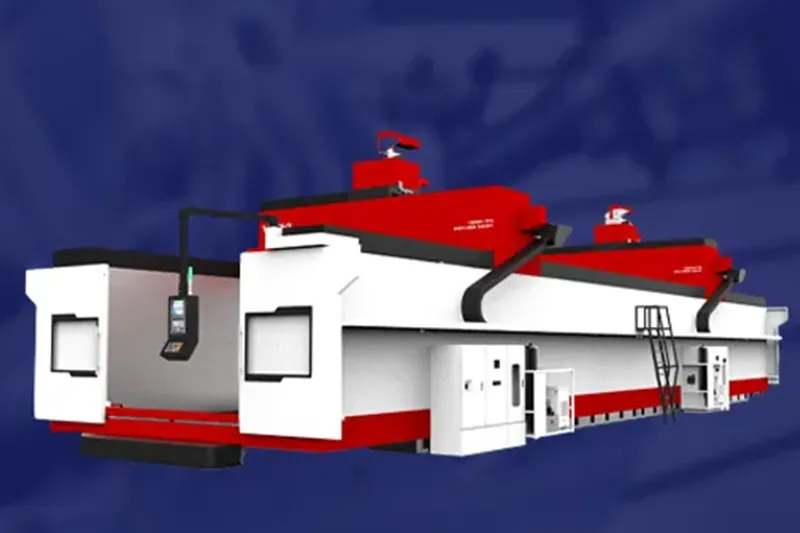
| Model | Travel X/Y/Z (mm) | Table size (mm) | Max height (mm) | Spindle power | Rapid X/Y/Z (m/min) | Weight (t) |
|---|---|---|---|---|---|---|
| SP4025HPG | 4200 / 2500 / 1200 | 4000 x 2100 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 42 |
| SP6025HPG | 6200 / 2500 / 1200 | 6000 x 2100 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 52 |
| SP6030HPG | 6200 / 3000 / 1200 | 6000 x 2600 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 58 |
| SP8030HPG | 8200 / 3000 / 1200 | 8000 x 2600 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 70 |
| SP12030HPG | 12200 / 3000 / 1200 | 12000 x 2600 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 115 |
| SP4035HPG | 4200 / 4000 / 1200 | 4000 x 1800 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 48 |
| SP6035HPG | 6200 / 4000 / 1200 | 6000 x 1800 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 58 |
| SP8035HPG | 8200 / 4000 / 1200 | 8000 x 2600 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 70 |
| SP12035HPG | 12200 / 4000 / 1200 | 12000 x 2600 | 1500 (custom) | 28/42 kW (gearbox 1070/1604 Nm) | 20 / 20 / 20 | 115 |
Note: Split-style HPG frames are built to order; X-axis travel can be extended up to 60 m and Y/Z to 8 m / 3 m. Control: SIEMENS 828D / 840D.
Specifications
SP Series Specifications
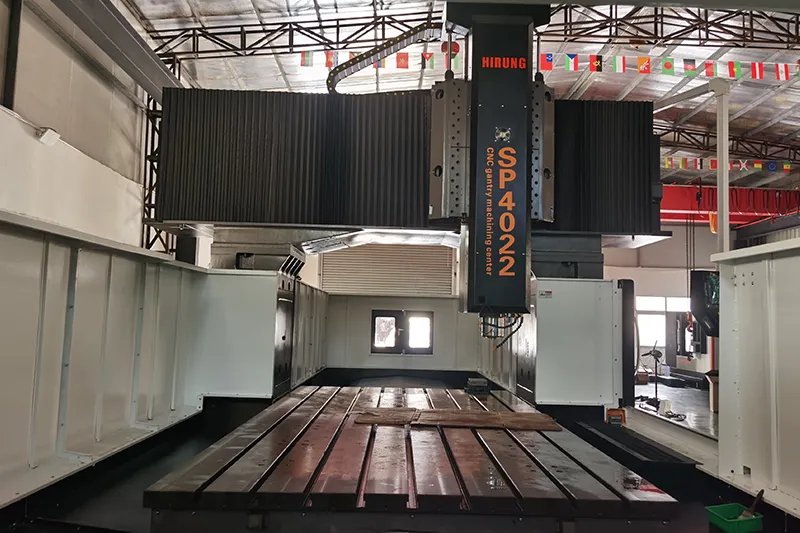
| Model | Travel X/Y/Z (mm) | Max table load (kg) | Spindle | Power (kW) | Positioning / repeat (VDI 3441) |
|---|---|---|---|---|---|
| SP1615 | 1600 / 1500 / 800 | 4000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
| SP2515 | 2700 / 1650 / 800 | 5000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
| SP3022 / 4022 | 3000-4000 / 2200 / 1000 | 9000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
| SP4025 | 4000 / 2500 / 1000 | 12000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
| SP4030 | 4000 / 3000 / 1200 | 15000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
| SP6039 | 6000-24000 / 3900 / 1200 | 20000 | BT50, 8000 rpm belt | 15/18.5 (FANUC) – 22 (SIEMENS) | 0.01 / 0.005 mm per 1000 mm |
Note: SP spindle supports optional direct-drive or gearbox. Rapid traverse X/Y up to 24 m/min (model dependent). Automatic angle head (1 deg / 5 deg division, 10 s switch) optional for 5-sided machining.
HIRUNG Gantry
Features of Our CNC Gantry Machining Centers
Every HIRUNG gantry center is built around four engineering pillars that protect accuracy under heavy cutting: an ultra-rigid cast-iron base, verified geometric accuracy, the right guideway mix for speed and force, and active thermal control. The sections below detail the components buyers ask about most.
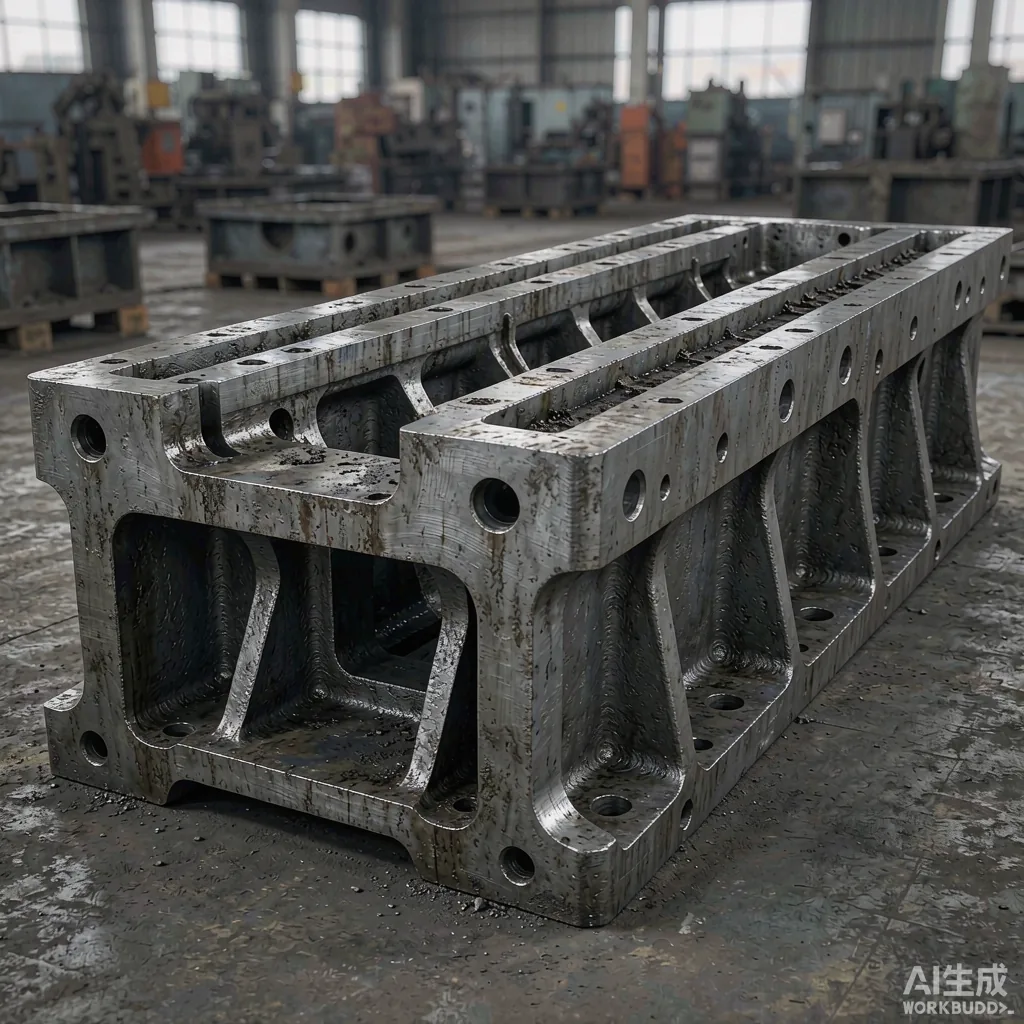
Ultra-Rigid Mechanite Cast Iron Foundation
Both series use high-grade Mechanite cast iron (FC300 / GC-275 class) that is annealed to relieve internal stress before machining. Stiffened Y-axis beams and a secret alloy formula (with Cr, Ni, Mo, Cu and Ti additions) give the frame the damping needed for vibration-free heavy milling and a long, stable service life.
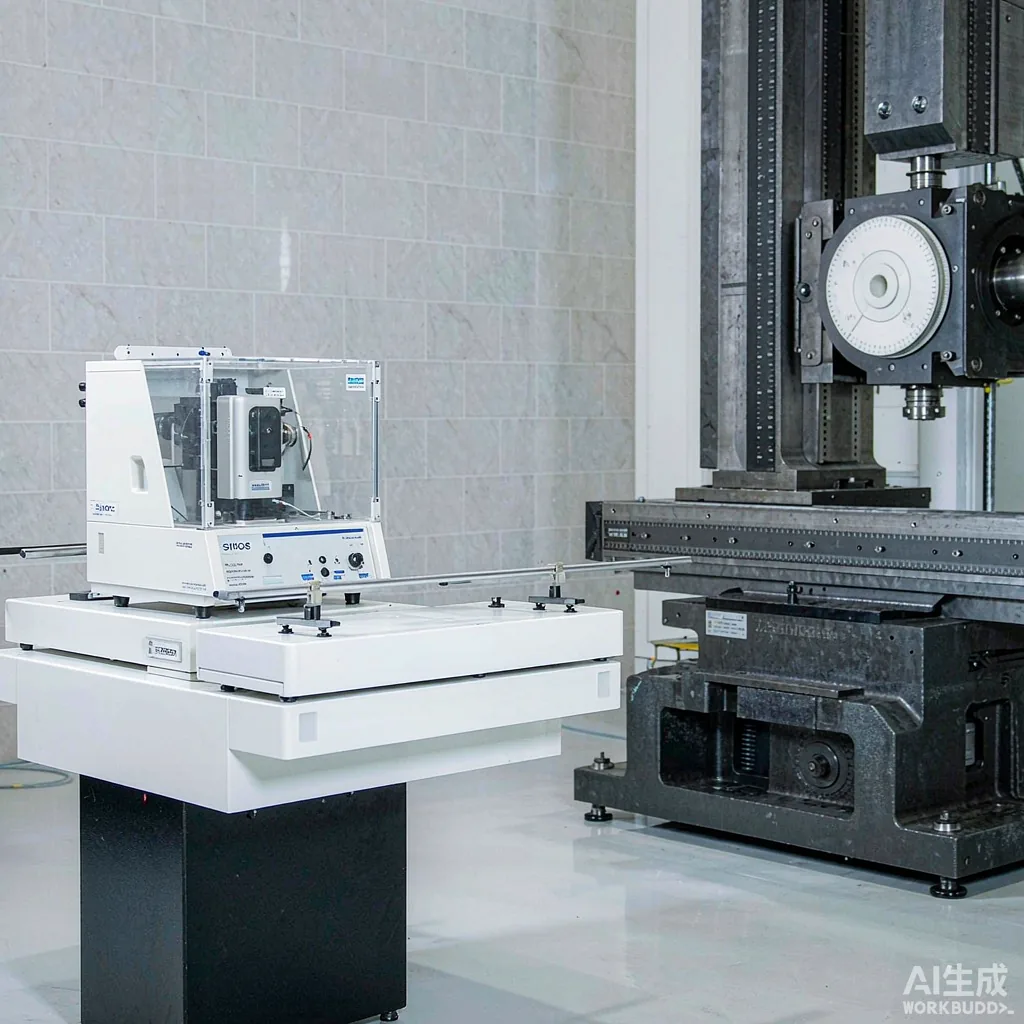
Micron-Level Geometric Accuracy
Each gantry is verified with laser interferometer and ballbar testing. HIRUNG guarantees positioning accuracy of <=0.01 mm over full travel and repeatability of +/-0.003 mm; the SP series is certified to VDI 3441 at 0.01 mm / 1000 mm positioning and 0.005 mm / 1000 mm repeatability. This is the precision required for large structural parts and high-precision molds.
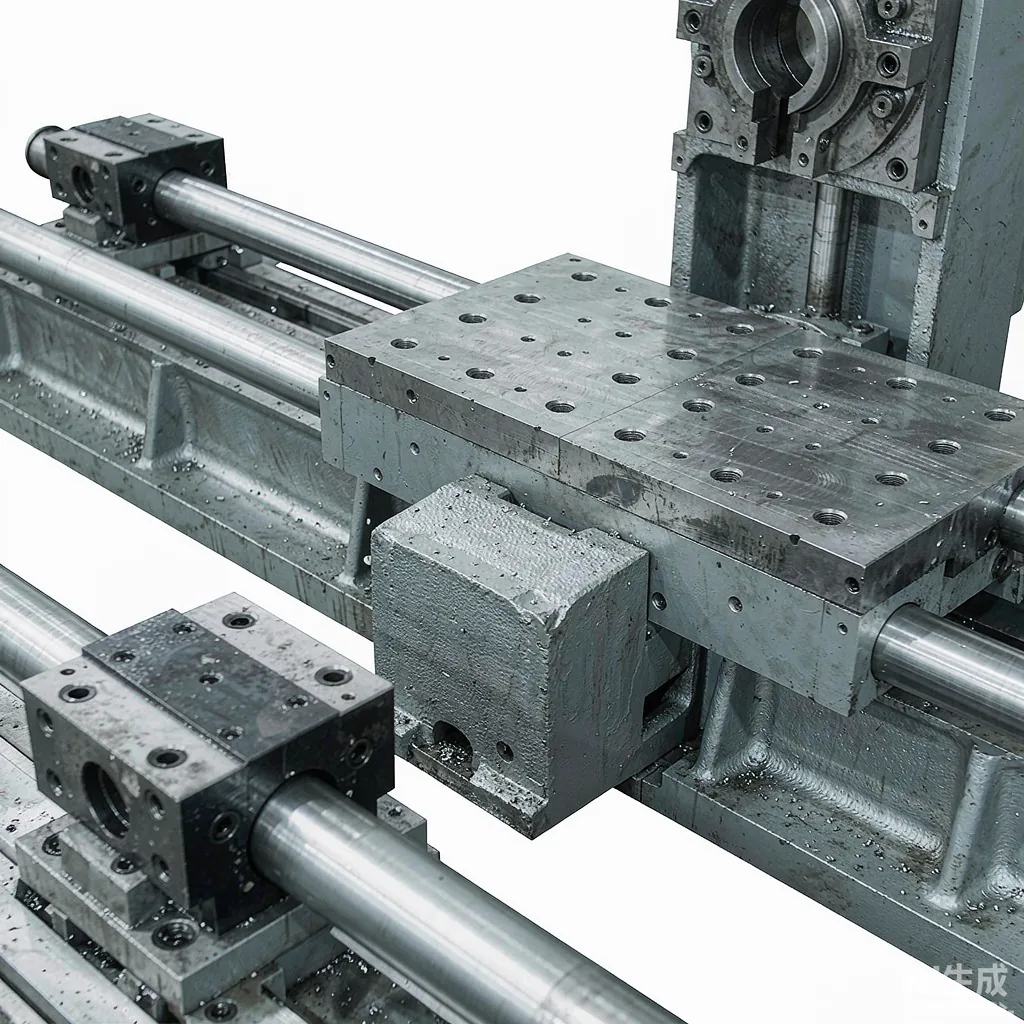
Box-Way & Linear Guide Hybrid Optimization
To balance speed and cutting force, HIRUNG tailors the guideway layout per model. Hardened box-ways (HRC 50+) absorb the heavy milling loads, while premium linear guideways (THK / HIWIN roller guides) deliver rapid traverse up to 20-24 m/min and the dynamic response needed for intricate 3D surfaces. The HPG Z-axis uses four roller guides for extra rigidity.
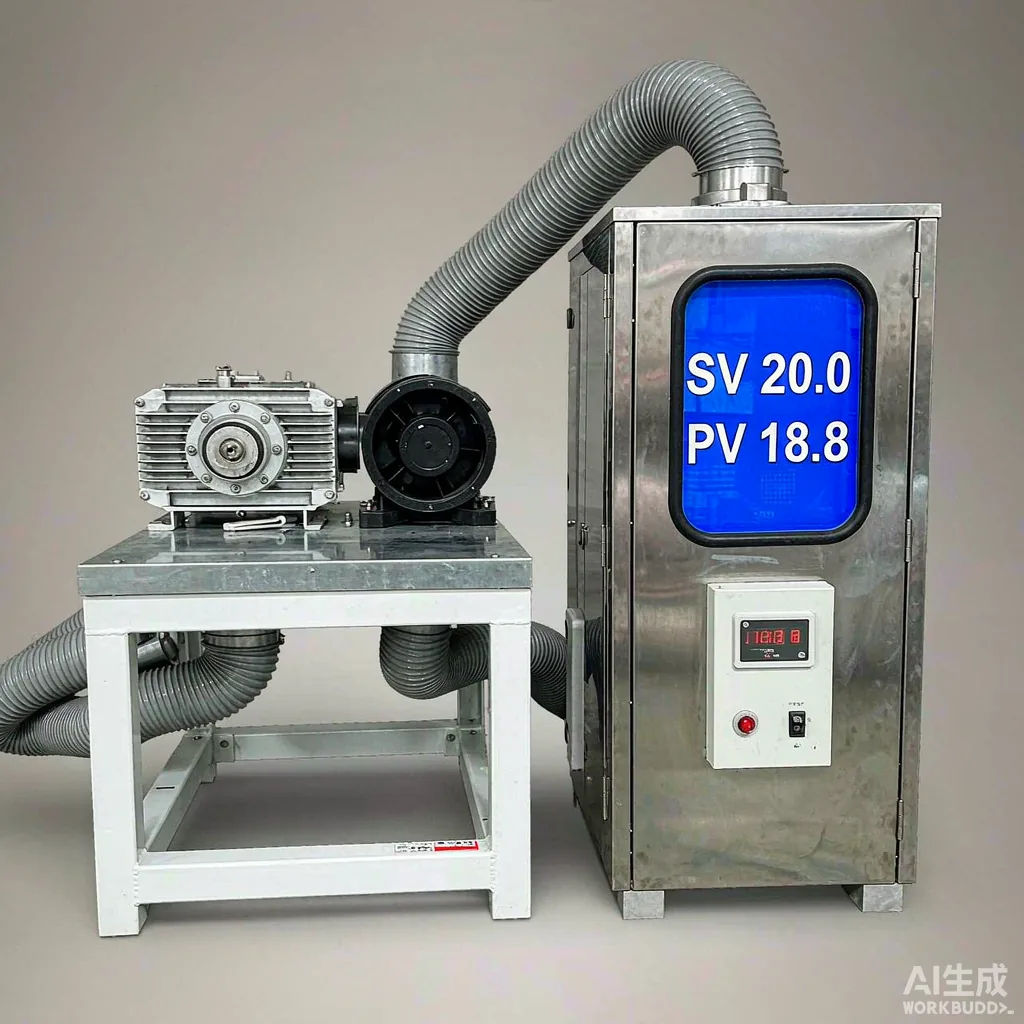
Advanced Thermal Stability Control
A spindle oil-cooling system is standard, holding the core of the machine at constant temperature. Active cooling keeps Z-axis thermal displacement within 0.005 mm, so the first part and the last part of a long run stay dimensionally identical – critical for unattended and multi-shift production.
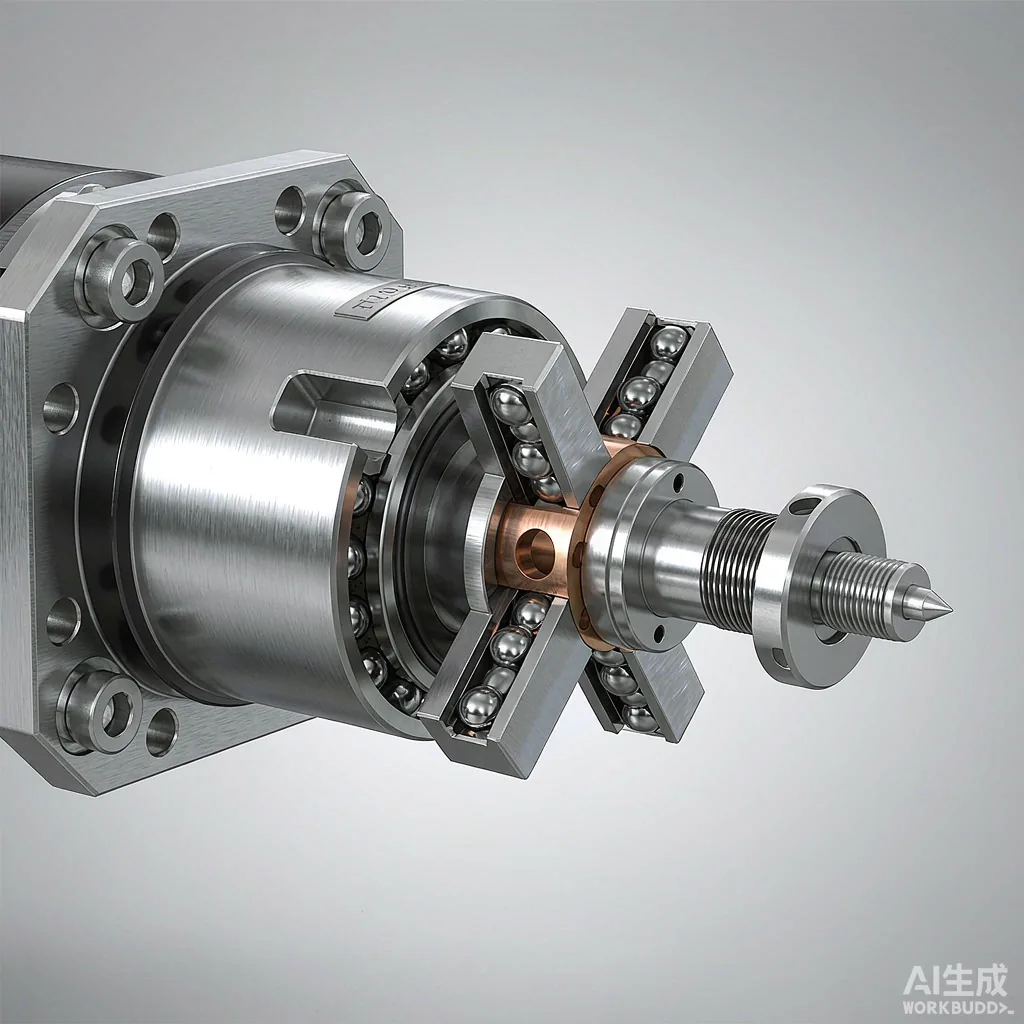
Heavy-Duty BT50 Spindle & Drivetrain
Taiwan-made BT50 spindles run on Japan NSK bearings for stability and durability. An optional Germany ZF gearbox pushes torque to 380 Nm for heavy cutting; the five-axis line uses Italian HSD and German TRAMEC spindles of 24-93 kW. C3 double-nut pre-tensioned ball screws (Japan P4 bearings) and KTR couplings keep the feed system rigid and long-lived.
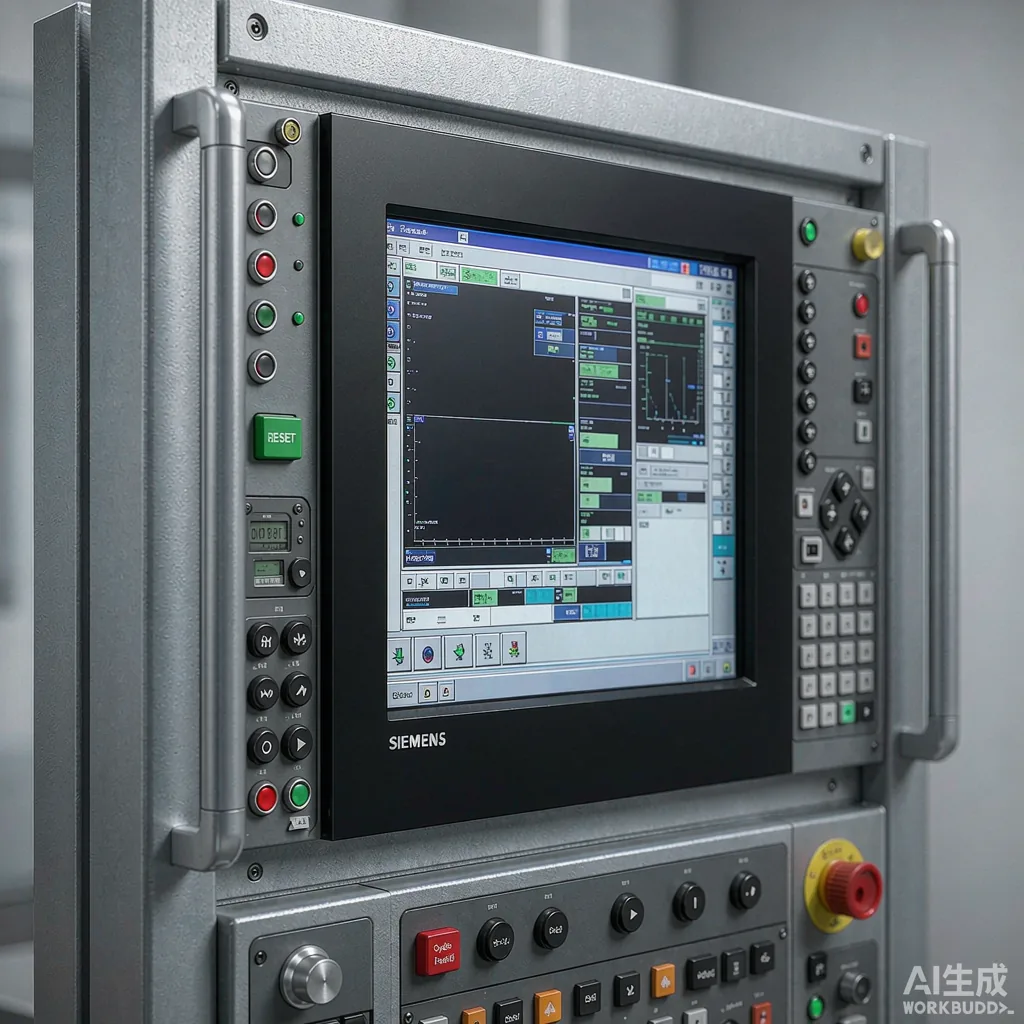
Trusted CNC Control Systems
SIEMENS 828D is the standard control, with SIEMENS 840D on five-axis models and HEIDENHAIN or FANUC 0i-MF available as options. Large memory handles the big programs needed for complex molds, and FAGOR optical scales can be added where the highest closed-loop accuracy is required.
Quality
Precision Manufacturing & Quality Assurance
HIRUNG treats accuracy as a process, not a inspection step. From casting to final scraping, every gantry passes documented controls so the machine you receive matches its spec sheet for decades.
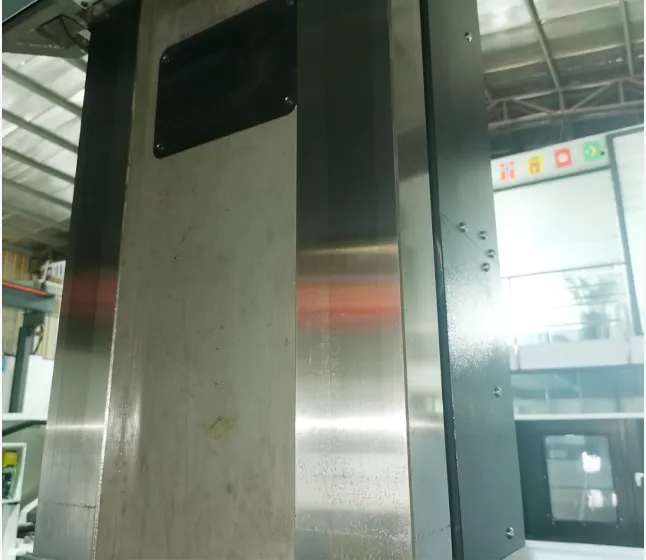
Precision Manufacturing & Ultra-Rigid Assembly
The foundation is Mechanite GC-275 cast iron, stress-relieved for lifetime stability. Class C3 double-nut ball screws and premium roller guides hold structural alignment within 0.01 mm / 1000 mm, and every critical interface is hand-scraped so the machine sits flat and vibration-free under load.
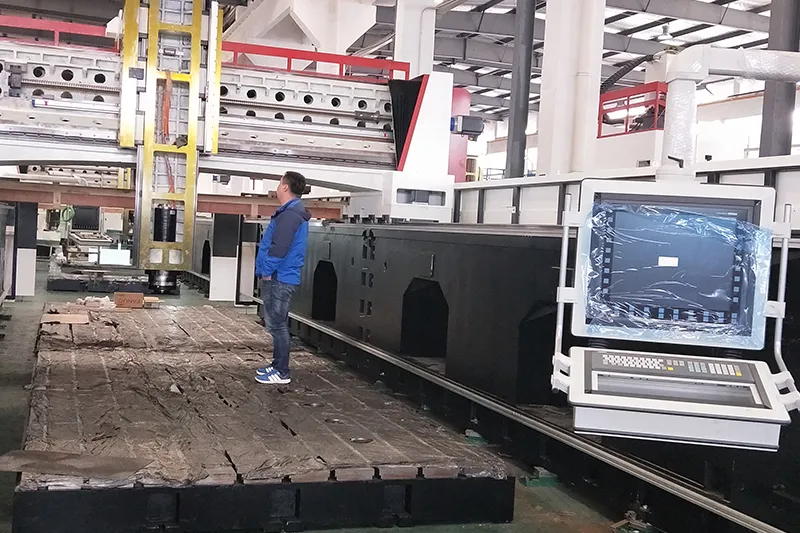
Industry-Leading Accuracy Testing
Every machine passes dual-stage verification with Renishaw laser interferometers and wireless ballbar tests to calibrate full-travel pitch error and geometric squareness: positioning accuracy <=0.010 mm (full travel), repeatability +/-0.003 mm, and thermal displacement <0.005 mm via active oil cooling.
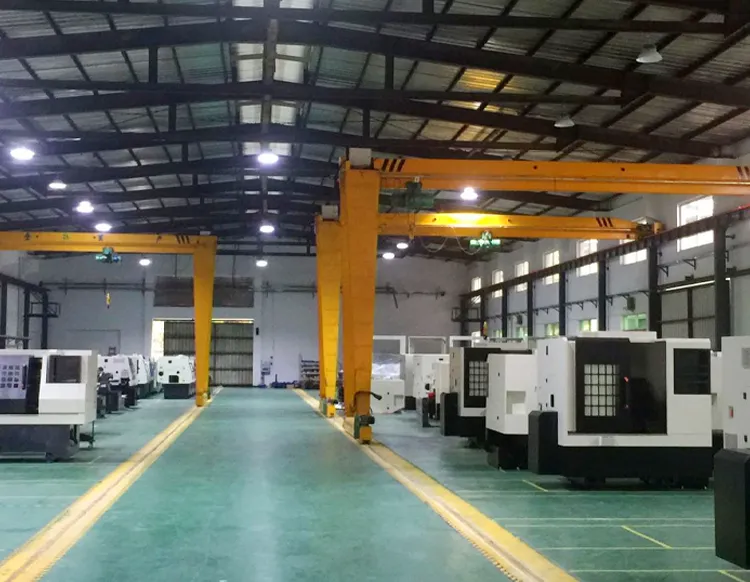
Casting & Stress-Relief Process
HIRUNG follows a strict annealing procedure to release internal stresses in the cast iron before machining. The full sequence – casting, tempering, rough machining, fine machining, painting, finish machining, then packaging – plus a controlled alloy recipe is what keeps the frame dimensionally stable for its whole working life.
HIRUNG Gantry
Why Choose HIRUNG Gantry Centers?
Beyond the spec sheet, HIRUNG gantry centers are chosen for predictable uptime, global support and a lower cost of ownership over the machine lifetime.
Proven Global Reliability
Exporting since 2015, HIRUNG has installed gantry centers in over 33 countries, including high-precision markets such as Sweden and Russia. Manufacturing standards exceed the domestic average and deliver roughly 30% longer machine lifecycle.
Superior Heavy-Duty Performance
Mechanite GC-275 cast iron and dual-drive Y-axis synchronization let the gantry handle table loads up to 30 tons (HPG effectively unlimited) while holding positioning accuracy of <=0.01 mm – the combination heavy industry needs for continuous cutting.
Precision That Lasts
Micron-level repeatability (+/-0.003 mm) plus active spindle oil cooling keep thermal displacement under 0.005 mm, so your first part is as precise as your ten-thousandth – year after year.
Lower Total Cost of Ownership
Modular components and high-durability wear parts make maintenance straightforward, cutting downtime and long-term service cost. Reliable accuracy also means less scrap and rework across the machine lifetime.
HIRUNG Gantry
Applications
HIRUNG gantry centers serve industries where part size, rigidity and accuracy all matter at once. Typical applications span tooling, flight structures, energy hardware and life-critical components.
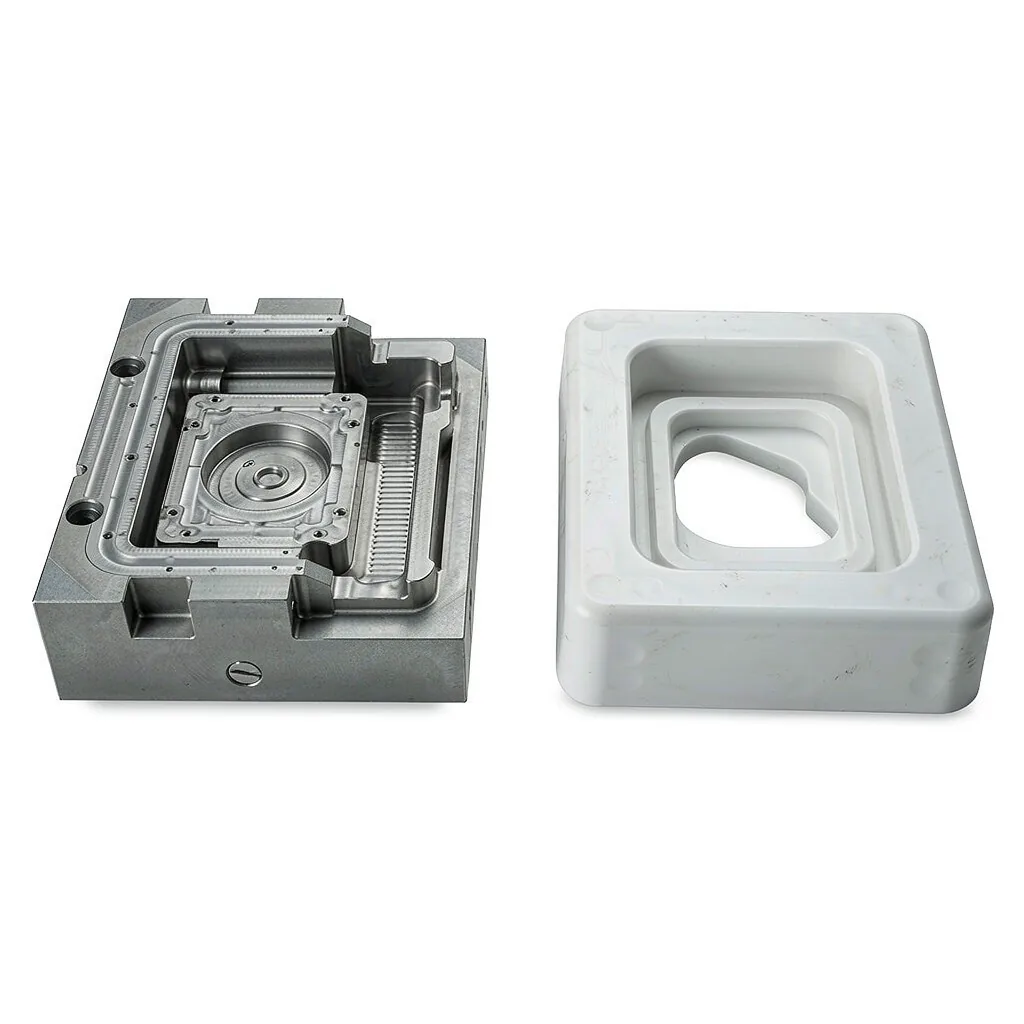
Mold & Die
Ultra-rigid Mechanite structures and active thermal control deliver mirror-class finishes for molds and dies at +/-0.003 mm repeatability and <0.005 mm Z-axis stability – the basis for a flawless molded surface.
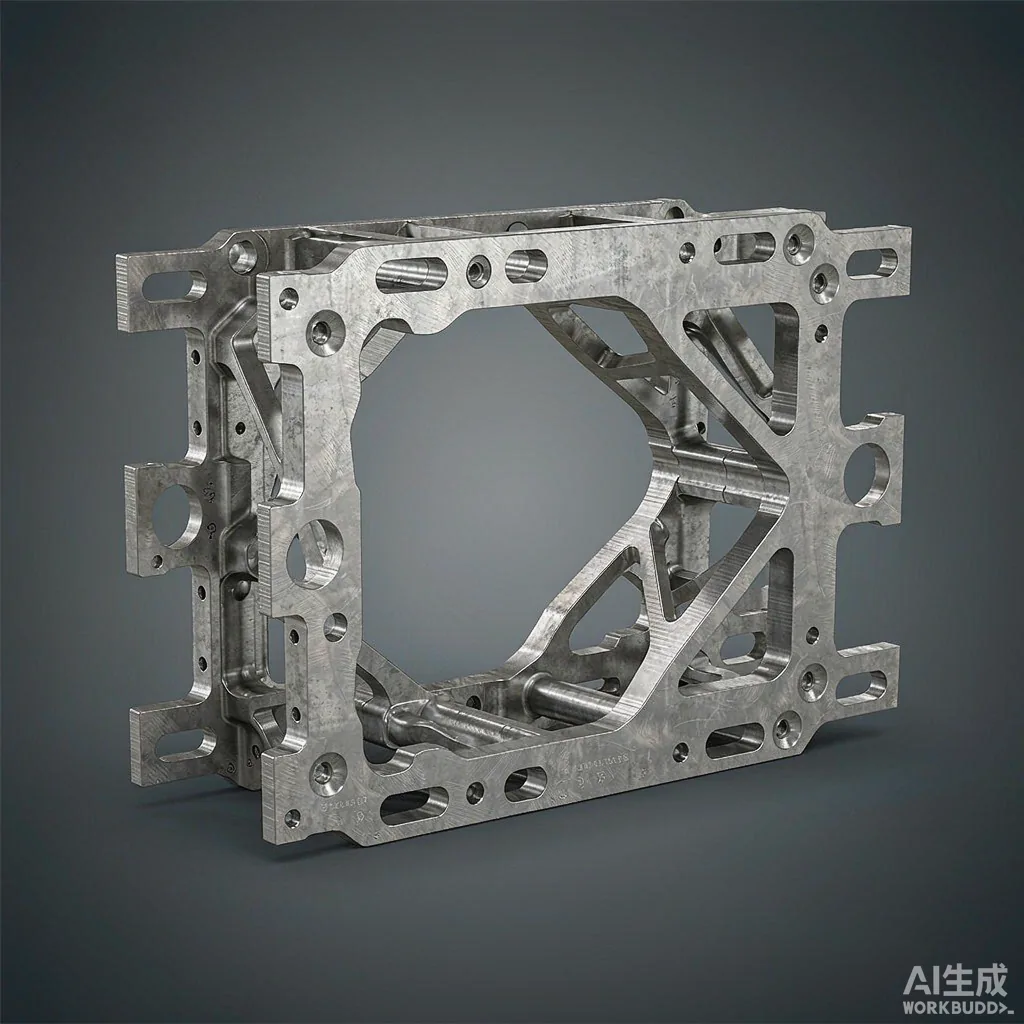
Aerospace
Dual-drive synchronization and laser-calibrated precision give aerospace-grade integrity for complex, high-strength structural parts: <=0.01 mm positioning and +/-0.003 mm repeatability on large panels and frames.
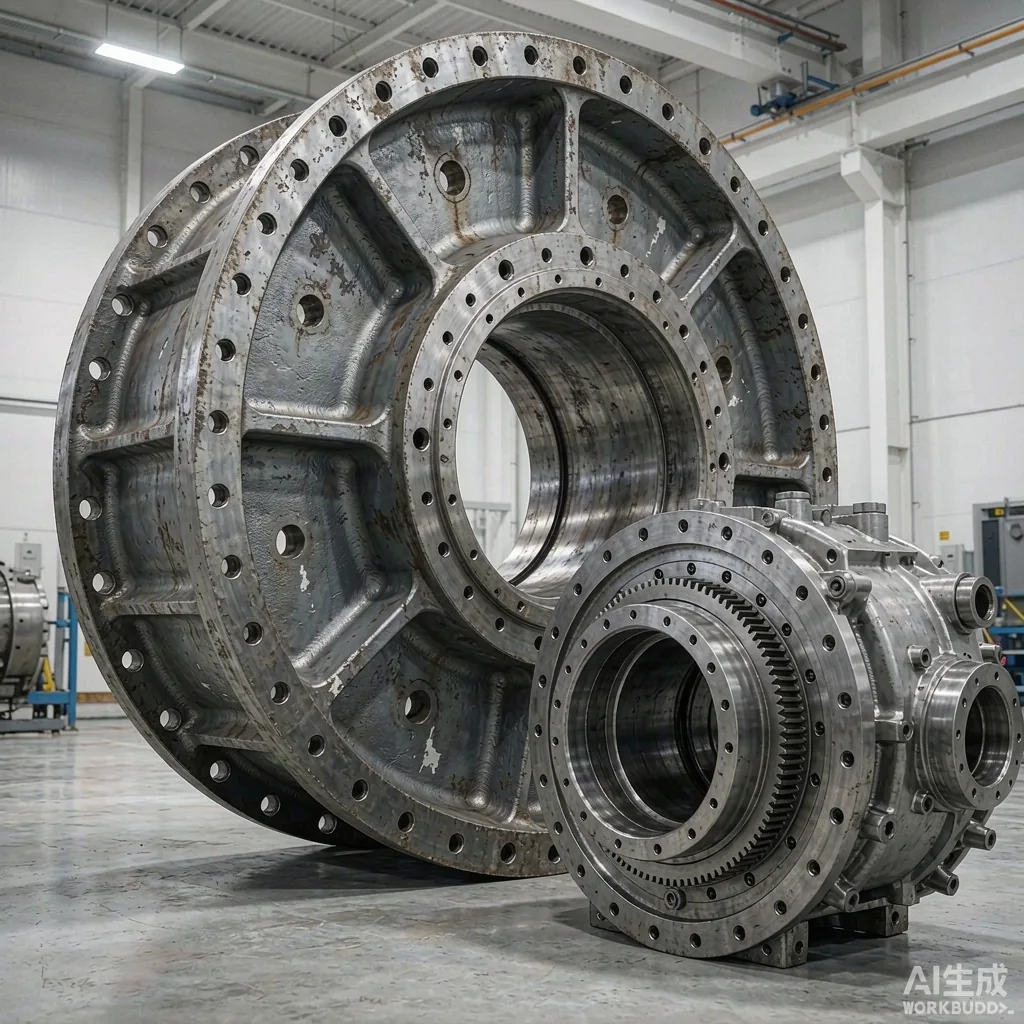
Energy & Heavy Equipment
The HPG column-moving structure is built for massive energy-equipment and shipbuilding components where table load is effectively unlimited and X-axis travel can reach 12 m (custom up to 60 m). This is where a double-column gantry replaces a floor mill.
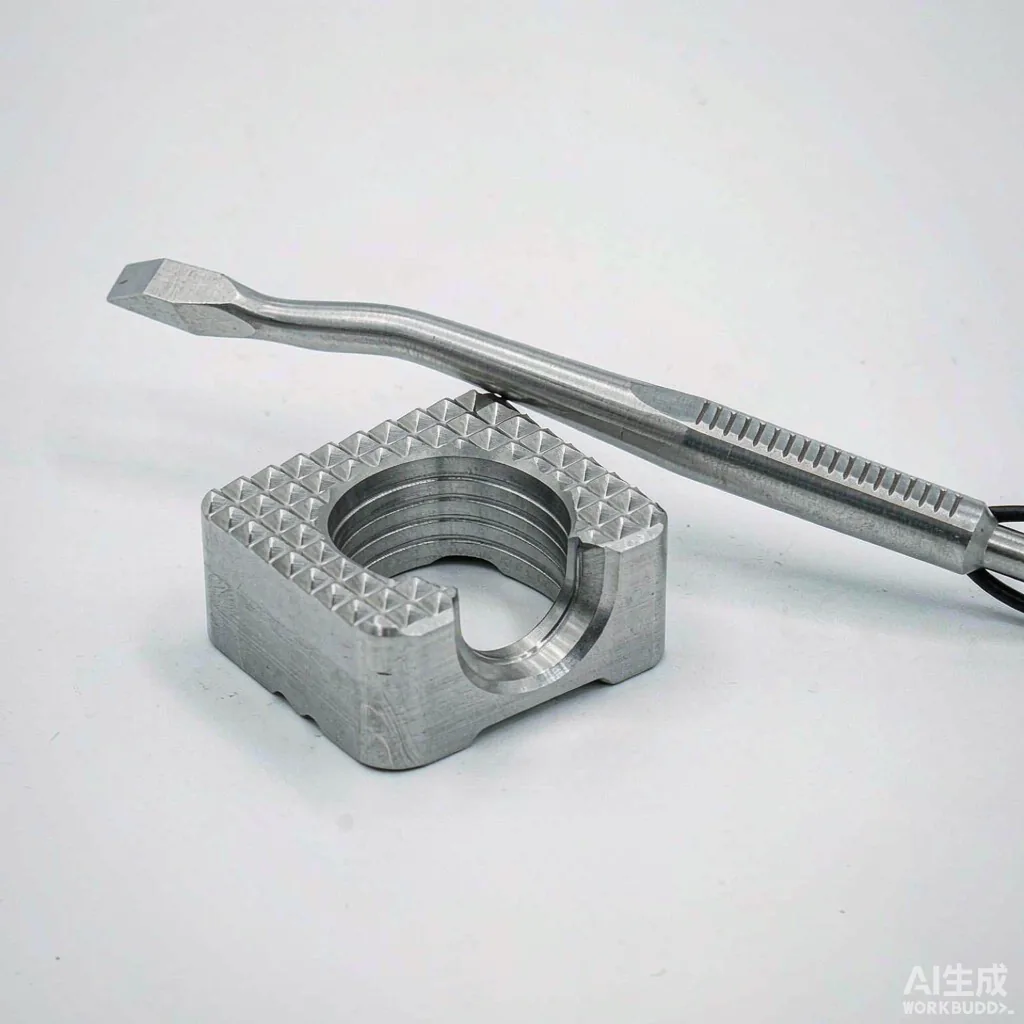
Medical Instruments
Micron-level motion control guarantees the strict dimensional integrity required for life-critical medical instruments: +/-0.003 mm repeatability and <=0.01 mm positioning on small, complex, high-value parts.
Automotive & General Machining
From fixtures and body dies to general large-part machining, the SP and HPG ranges cover high-mix automotive tooling and job-shop work where rigidity, speed and uptime decide profitability.
Built to order
Customization & Capacity
Standard HPG and SP models cover most requirements, but HIRUNG regularly builds to order. Split-style HPG frames extend X-axis travel up to 12,000 mm (custom up to 60 m), Y up to 8 m and Z up to 3 m, with table width and height tailored to your parts. Share your part drawings and we return a selection plan and quotation.
FAQ
FAQ
Contact our sales team with the required model, configuration and the drawings of the parts you plan to machine. Our engineers prepare a selection plan and a quotation, then we sign a sales contract once the specification is confirmed.
Settlement can be in USD, EUR or RMB. We accept T/T and L/C. The usual terms are a 30% production deposit with the remaining 70% paid before shipment.
Standard models are typically delivered within 30 days; some are in stock. Specially customized equipment is built within 180 days depending on scope.
HIRUNG has exported since 2015 and uses a mature, fully protected packaging solution suited to long international shipping, so the machine arrives ready to install.
Pick the HPG column-moving gantry when part weight or length dominates – load is effectively unlimited and X-travel can reach 60 m. Pick the SP table-moving gantry when surface finish, repeatability and rigidity matter most, such as molds, aerospace parts and medical instruments.
Positioning accuracy is <=0.01 mm over full travel with repeatability of +/-0.003 mm; the SP series is verified to VDI 3441 at 0.01 mm / 1000 mm positioning and 0.005 mm / 1000 mm repeatability. Thermal displacement is held under 0.005 mm by active oil cooling.
Yes. Split-style HPG frames are built to order, extending X-axis travel up to 12,000 mm (custom up to 60 m), Y up to 8 m and Z up to 3 m, with table width and height tailored to your workpiece.
SIEMENS 828D is standard, with SIEMENS 840D on five-axis models. HEIDENHAIN and FANUC 0i-MF are offered as options, and FAGOR optical scales can be added for closed-loop accuracy.
Get started
Talk to a Gantry Specialist
Tell us your part size, material and tolerance, and HIRUNG engineers will recommend the right HPG or SP configuration – with a selection plan, quotation and delivery schedule. Explore the HPG series (column moving) and the SP series (table moving) for model detail, or contact our team to start your project.