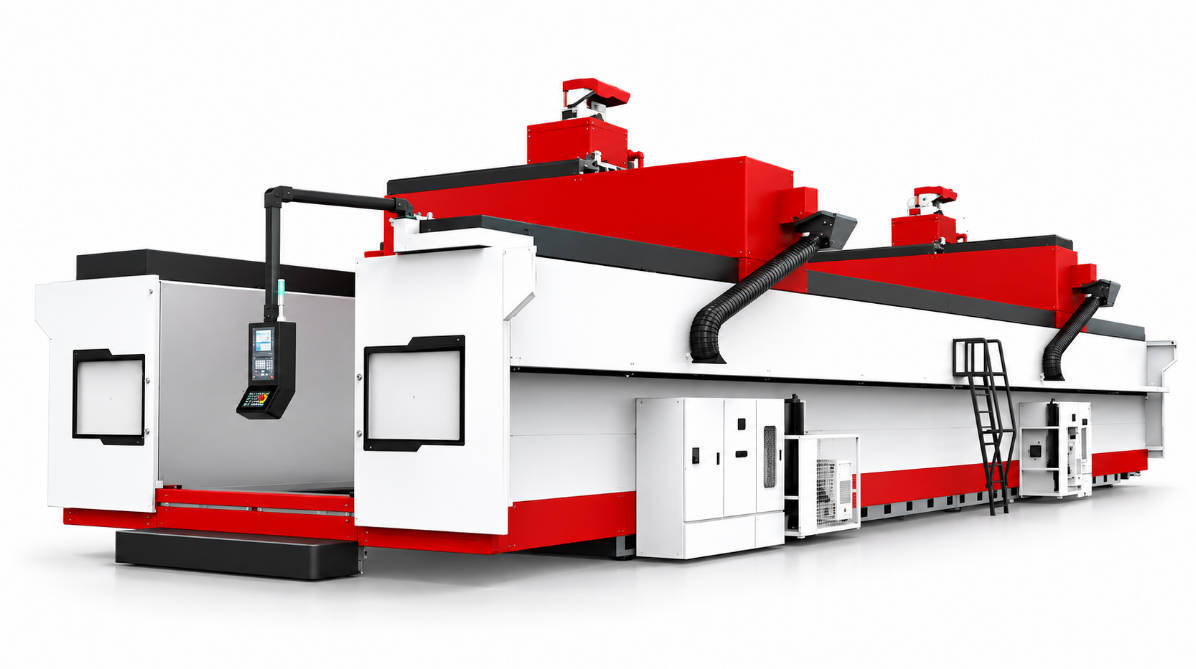
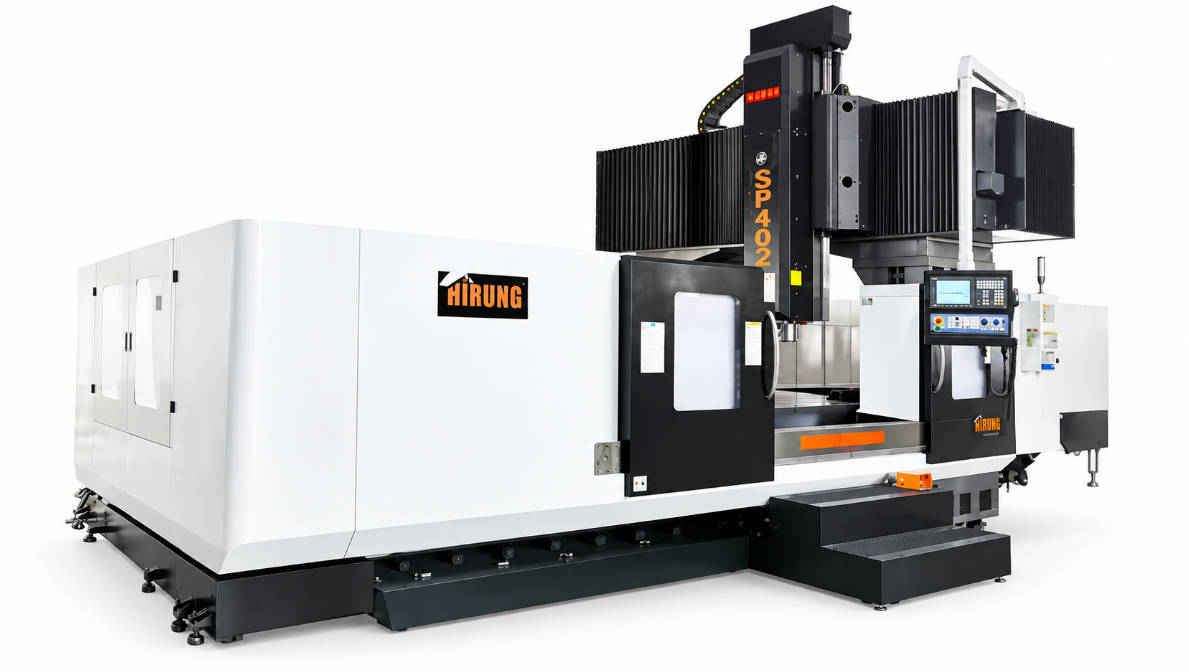
A CNC gantry machine’s accuracy is the result of a chain of design and manufacturing decisions — base rigidity, guideway type, beam and crossbeam design, ball-screw quality, spindle thermal control, the control system, and assembly precision. In short, the accuracy of a CNC gantry machine is determined less by a single component and more by how well the structure, drive, spindle, and control system work together to resist deflection, heat, and vibration during a cut.
If you are evaluating a CNC gantry machine for large-part machining, understanding these factors helps you read a specification sheet critically and ask the right questions before purchase.
What “Accuracy” Means for a CNC Gantry Machine
Before listing the factors, it helps to separate two terms that are often confused. Positioning accuracy describes where the tool actually ends up relative to the program point, while repeatability describes how consistently the machine returns to the same point. A machine can be highly repeatable yet still systematically off; both matter for heavy-equipment and precision parts.
Positioning Accuracy vs Repeatability
On a well-built gantry, positioning accuracy is typically specified at ≤ 0.010 mm over full travel, with repeatability around ± 0.003 mm. Those numbers are only meaningful if the structure behind them is engineered to hold them under load and over time. A repeatable machine may still need offset calibration to be accurate; a machine that is neither repeatable nor accurate cannot be relied on for interchangeable, fit-to-print parts.
Why Accuracy Matters to the Buyer
For heavy and large-part manufacturing, accuracy failures show up as scrap, rework, and assembly problems downstream. A bore that is a few hundredths of a millimeter out can stop a gearbox from seating. Mounting faces that drift across a long weldment create shimming and fit-up labor. A Mehanite cast-iron base provides the mass and internal damping that keep a gantry stable under heavy cuts — which is why base design is the first factor worth examining.
The cost is not only the rejected part. A dimension that is consistently off by a small amount forces downstream rework, extra fixtures, or field shimming — all of which raise the true cost per good part. For contract manufacturers, that hidden cost is often larger than the machine’s purchase price over its working life.
Factor 1: Base and Bed Rigidity
The base is the foundation of everything above it. The largest gantry machines in HIRUNG’s range are built on a high-grade Mehanite cast iron base (commonly referenced as FC300 / GC-275 grades), heat-treated and stress-relieved so the material does not continue to move after installation. Cast iron’s internal damping absorbs vibration that would otherwise transmit into the cut.
The practical takeaway: ask whether the base is stress-relieved, and how the manufacturer controls residual stress. A base that warps months after installation will quietly erode accuracy.
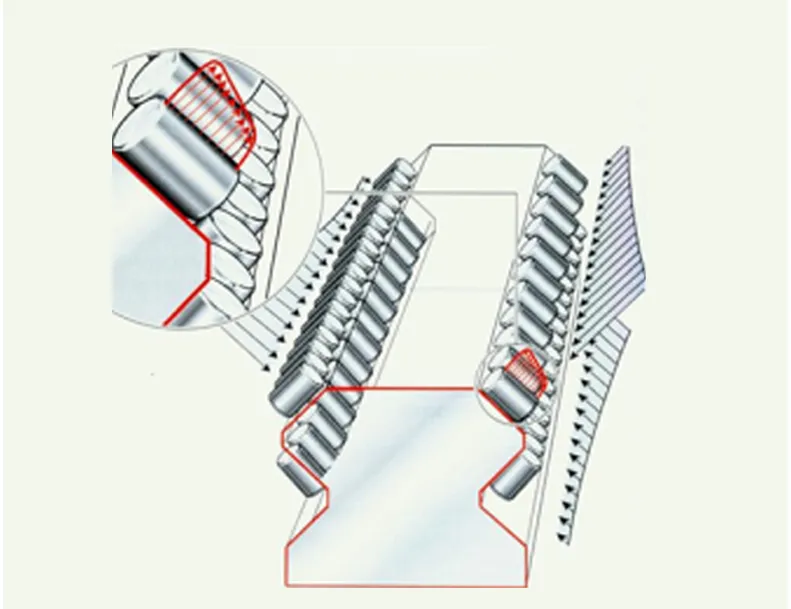
Factor 2: Guideways — Box-Way vs Linear Guide
Guideways define how the moving axes resist cutting force. The two common choices trade rigidity for speed differently.
| Guideway type | Strength | Trade-off | Typical use on a gantry |
|---|---|---|---|
| Box ways (sliding) | High damping, excellent under heavy stock removal | Lower rapid traverse | Heavy milling, roughing of large castings |
| Linear guideways (roller) | High speed, low friction, fast traverse | Less damping under very heavy loads | Finishing, faster cycle work |
HIRUNG uses hardened box ways (typically HRC 50+) where heavy milling damping is needed, and premium roller guideways where rapid traverse up to roughly 20 m/min is the priority. The right choice depends on whether your parts are finish-critical, stock-removal-heavy, or both.
Factor 3: Beam and Crossbeam Design
In a gantry, the crossbeam carries the spindle, so its stiffness directly limits how far the tool can deflect under side load. A double-column layout keeps forces symmetric, while a box-in-box crossbeam section raises torsional rigidity without an oversized mass penalty.
Column-Moving vs Fixed-Bridge Layouts
The HIRUNG HPG series uses a column-moving design with a fixed table, well suited to extra-large and very heavy workpieces where the table load is effectively unlimited. By contrast, the HIRUNG SP series uses a fixed-bridge, table-moving design that maximizes rigidity for finishing accuracy. Both share the principle that the beam must resist bending and torsion while the spindle applies side load.

Factor 4: Ball Screws and Drive Systems
The drive train converts control commands into actual motion. Class C3 double-nut ball screws, preloaded to remove backlash, are a common specification for precision gantry machines because they hold position under reversing loads. Premium roller guides in the axis supports complement the screws by keeping the carriage aligned.
When comparing quotes, look at the ball-screw grade and preload method, not just the rated feed rate. A low-grade screw may look fast on paper yet drift under real cutting loads.
Factor 5: Spindle and Thermal Control
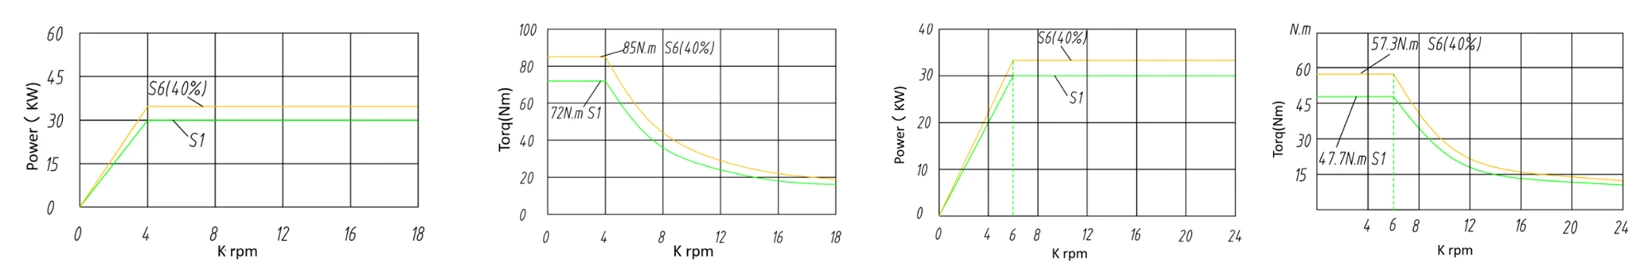
Heat is the quiet enemy of accuracy. As the spindle warms, it grows; that growth pushes the tool away from the programmed position. Active spindle oil cooling is the single most effective way to control the thermal growth that otherwise shifts accuracy. On HIRUNG gantry machines, an oil-cooling system is fitted as standard, and thermal displacement is controlled to below 0.005 mm.
Beyond the spindle, coolant temperature, ambient swings, and even hydraulic lines contribute to drift. A machine that manages spindle heat but ignores the rest will still lose accuracy over a long shift.
Factor 6: Control System and Calibration
The control system does more than run G-code. Modern controllers compensate for leadscrew error, reverse backlash, and — in higher-end setups — volumetric and thermal error. But compensation is only as good as the data behind it.
Every HIRUNG machine is verified with Renishaw laser interferometer and ballbar testing before shipment. These measurements map the machine’s actual geometric and positioning behavior, which is the basis for any controller compensation. Ask a supplier to show the laser and ballbar report for a machine in your size class.
Factor 7: Assembly and Hand-Scraping
Two machines with identical castings can perform differently based on how they are assembled. Critical interfaces — ways, gibs, and bearing seats — are often hand-scraped to a contact pattern that a machined surface alone cannot guarantee. Hand-scraping the critical interfaces is what lets a gantry hold structural alignment within 0.01 mm per 1000 mm. It is slow, skilled work, but it is a major reason precision holds up in the field rather than only on the showroom floor.
Factor 8: Foundation and Environment
No machine is better than the floor it sits on. A gantry generates high static and dynamic loads, so the foundation must support machine weight, workpiece, and cutting forces without settling. Temperature stability in the shop also matters; large parts and machines respond to daily thermal cycles.
Accuracy Factors at a Glance
| Factor | What it primarily controls | What to verify with the supplier |
|---|---|---|
| Base / bed | Vibration damping, long-term stability | Cast iron grade, stress-relief process |
| Guideways | Load resistance vs traverse speed | Box-way vs linear, hardness, preload |
| Crossbeam | Torsional rigidity under side load | Beam section design, double-column layout |
| Ball screws | Position hold under reversing load | Grade (e.g., C3), double-nut preload |
| Spindle | Thermal growth during the cut | Oil cooling, measured thermal drift |
| Control | Error compensation quality | Laser / ballbar verification report |
| Assembly | Geometric alignment | Hand-scraping of critical interfaces |
| Foundation | Load support, settling | Floor drawing, environmental plan |
How to Read an Accuracy Specification
Accuracy figures only mean something when you know the conditions. A positioning number quoted under light load on a single axis is not the same as accuracy during a multi-axis heavy cut. Good suppliers state the measurement standard, the load condition, and the temperature at which the result was obtained. A specification without a stated measurement method should be treated as marketing, not as a guarantee of shop-floor performance.
Common Mistakes When Evaluating Accuracy
- Reading only the catalog accuracy number. The figure is only valid under the conditions the builder tested; ask how it was measured.
- Ignoring spindle thermal control. A machine that is accurate cold may drift within the first hour of running.
- Overlooking the foundation. A perfect machine on a weak floor will still lose geometry.
- Confusing repeatability with accuracy. Consistency is not the same as correctness.
- Skipping witnessed run-off. A measured run-off on a part like yours is worth more than a brochure claim.
How to Choose the Right Machine and Supplier
Selecting for accuracy means matching the machine to your parts, then verifying the claims. Useful checkpoints include:
- Request positioning accuracy and repeatability figures with the measurement method.
- Ask for the laser interferometer and ballbar report for a comparable machine.
- Confirm guideway type against your roughing vs finishing mix.
- Review the crossbeam and base design for your largest, heaviest part.
- Confirm the foundation and environmental requirements before installation.
For heavy, accuracy-sensitive work on a fixed bridge, the HIRUNG SP series offers a table-moving design rated up to 30,000 kg table load, pairing rigidity with a stable spindle path for finishing.
FAQ
What are the main factors that affect CNC gantry machine accuracy?
The main factors are base rigidity, guideway type, crossbeam design, ball-screw quality, spindle thermal control, the control system and its calibration, assembly quality such as hand-scraping, and the foundation or environment.
How does bed rigidity affect machining accuracy?
A rigid, damped base resists the cutting forces and vibration that cause deflection and chatter. A high-grade cast-iron base, properly stress-relieved, keeps the structure stable so accuracy holds through long or heavy cuts.
Does spindle heat really change gantry machine accuracy?
Yes. As the spindle warms it expands and shifts the tool position. Active spindle oil cooling controls this growth; on well-built gantry machines thermal displacement can be held below 0.005 mm.
Box-way or linear guideways: which is better for accuracy?
Neither is universally better. Box ways damp heavy cuts and suit roughing, while linear guideways allow faster traverse and suit finishing. The right choice depends on your mix of stock removal and surface-quality requirements.
How is CNC gantry accuracy verified before delivery?
Accuracy is typically verified with laser interferometer and ballbar testing, which map geometric and positioning errors. Request the report for a machine in your size class rather than relying on a single catalog number.
Can a poor foundation ruin gantry machine accuracy?
Yes. A gantry applies high static and dynamic loads, and a weak or settling floor will distort the machine geometry regardless of how well it was built. The supplier should provide a foundation drawing matched to your site.
Conclusion
CNC gantry machine accuracy is not one number on a spec sheet; it is the sum of base, guideways, beam, drive, spindle, control, assembly, and environment working together. When you evaluate a machine, verify the claims with measured data — laser and ballbar reports, guideway and base specifications, and a witnessed run-off on a part like yours.
To discuss your accuracy requirements, review part drawings, or arrange a measured demonstration, contact the HIRUNG team or explore the CNC gantry machine range.